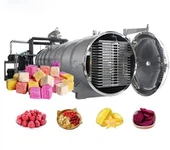
To pursue higher daily throughput, some factories compress time‑gap between production batches as much as possible. Right after one batch finishes, they load next‑batch materials and start new run immediately. Nevertheless, batch‑interval covers more than discharging and tray‑loading. It also includes equipment‑status recovery, inspection and necessary cleaning. Excessively compressed interval will bring multiple hidden risks.
Core tasks to be finished during batch‑interval after one production run: first, discharge finished goods and inspect trays & racks for residues and sticky materials; second, visual‑inspect chamber‑door sealing strip and valve status; third, check frost‑build‑up condition on cold‑trap and judge whether defrosting is required; fourth, perform necessary partial cleaning; fifth, confirm sensor readings are normal.
If defrosting is skipped: thick frost‑layer accumulates on cold‑trap and degrades water‑capturing capacity. Next‑batch sublimation efficiency drops, cycle extends and product quality becomes unstable. If sealing‑strip visual‑inspection is omitted, debris stuck on rubber strip will trigger vacuum‑leakage for subsequent batch.
Batch‑interval duration is not fixed value and depends on raw‑material categories: ① Low‑residue fruits & vegetables: little residue and light cold‑trap frost‑build‑up allow relatively short interval. ② High‑fat meat & seafood: volatile oil deposits on cold‑trap. Defrosting and focused cleaning shall be arranged every several batches, so sufficient turn‑around time must be reserved. ③ Frequent multi‑product change‑over: cleaning & purging procedure must be added into batch‑gap, which obviously lengthens turn‑around time.
Scientific planning logic: do not blindly chase minimal batch‑gap. Include defrosting, inspection and cleaning into overall production scheduling according to processed‑material types. When calculating daily production capacity, take batch‑interval into total working‑hours, instead of only counting sublimation drying time. Short‑term output‑gain obtained by forced interval compression will be offset by higher reject‑rate and increased equipment‑failures in later‑stage operation.